Understanding CNC Lathe Machine Cutting Operations
CNC turning is a fundamental machining process used to create precise components from metal, plastic, and other engineering materials. Different cutting operations allow manufacturers to shape workpieces, create internal and external features, and achieve specified dimensions efficiently.
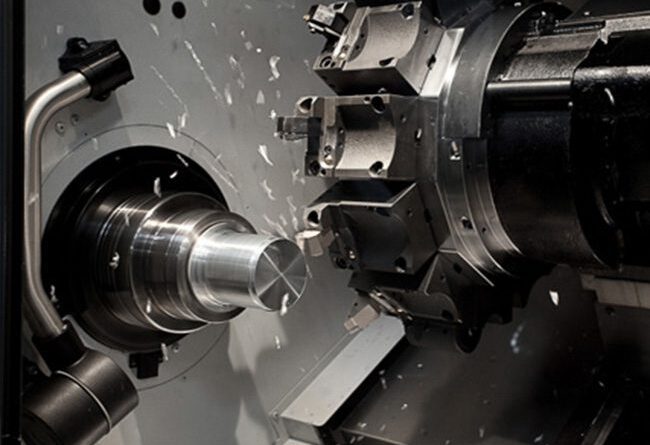
A CNC Lathe Machine uses programmed movements to coordinate the rotating workpiece with cutting tools. Understanding how individual cutting operations work can help manufacturers select appropriate tooling, machining parameters, and production methods.
What Are CNC Lathe Cutting Operations?
CNC lathe cutting operations involve removing material from a rotating workpiece using a controlled cutting tool. The tool follows a programmed path to produce the required geometry.
The choice of operation depends on the component design. A single part may require several operations, such as facing, rough turning, finish turning, drilling, and threading, before it reaches its final dimensions.
Facing
Facing is commonly performed at the beginning of a turning process. The cutting tool moves across the end of the rotating workpiece to create a flat surface.
This operation can establish a reference surface and prepare the component for subsequent machining. The tool path and feed rate should be selected according to the material and desired surface finish.
External Turning
External turning removes material from the outside diameter of a workpiece. It is one of the most common CNC lathe operations and can be used for both roughing and finishing.
Rough Turning
Rough turning focuses on removing material quickly. Larger depths of cut and suitable feed rates can be used when machine rigidity, tooling, and workpiece conditions allow.
The objective is generally to bring the workpiece close to its required shape while leaving sufficient material for finishing.
Finish Turning
Finish turning removes a smaller amount of material to achieve the final dimensions and surface quality.
Cutting speed, feed rate, tool geometry, and machine stability become particularly important during finishing because small changes can affect the final result.
Internal Turning and Boring
Boring enlarges or finishes an existing hole. A boring tool enters the workpiece and removes material from the internal surface.
Boring can be used to achieve accurate internal diameters and improve the geometry or surface finish of previously drilled holes.
Drilling
Drilling creates a new hole, typically along the spindle axis when performed on a conventional CNC lathe configuration.
Drill selection depends on the material, hole diameter, depth, and required accuracy. For deeper holes, chip evacuation and coolant delivery may require additional consideration.
Threading
Threading produces helical grooves on internal or external surfaces. CNC controls synchronize tool movement with spindle rotation to create the required thread pitch.
Threading parameters must be carefully programmed because incorrect synchronization or tooling can result in inaccurate thread geometry.
Grooving
Grooving creates a narrow recess on the workpiece. Grooves may be located on external diameters, internal surfaces, or faces depending on the component design.
Common applications include creating clearance areas, retaining-ring grooves, sealing features, and other functional recesses.
Parting and Cut-Off
Parting, also called cut-off, separates the finished component from the remaining stock. A narrow cutting tool moves radially into the rotating workpiece until the part is separated.
Proper tool alignment, cutting conditions, and chip control are important because parting can generate substantial cutting forces.
Chamfering
Chamfering removes a small amount of material from an edge to create an angled surface.
Chamfers can improve assembly, remove sharp edges, and provide a transition between different surfaces. They can usually be programmed as part of a larger turning sequence.
Taper Turning
Taper turning produces a gradual change in diameter along the length of a workpiece.
The CNC control can guide the cutting tool along a calculated path to create the required taper angle or dimensional transition.
Contour Turning
Contour turning is used when a component has a curved or irregular external profile rather than a simple cylindrical shape.
The cutting tool follows a programmed path based on the component’s geometry. Careful programming and appropriate tooling are important for maintaining dimensional accuracy along the entire contour.
Thread Relief and Undercutting
Some components require relief areas near shoulders or threaded sections. Undercutting creates a small recess that provides clearance for tools or mating components.
These operations are often included in detailed turning sequences and can help ensure that finished parts assemble correctly.
Roughing and Finishing Strategies
Many CNC turning programs separate material removal into roughing and finishing stages.
Roughing prioritizes efficient material removal, while finishing focuses on dimensional accuracy and surface quality. Separating these functions allows cutting parameters and tools to be optimized for each stage.
Choosing the Right Cutting Tool
Tool selection has a direct effect on machining performance. Factors to consider include:
- Workpiece material
- Type of cutting operation
- Required surface finish
- Cutting depth
- Feed rate
- Tool geometry
- Tool material and coating
Carbide inserts are widely used in CNC turning because they can support a broad range of machining applications, although other tool materials may be appropriate for specialized conditions.
The Role of Cutting Parameters
Spindle speed, feed rate, and depth of cut must be coordinated with the material and tooling.
Excessive cutting speed can increase heat and tool wear, while an unsuitable feed rate can affect surface finish and cutting efficiency. Depth of cut also needs to remain within the capabilities of the machine, workholding system, and cutting tool.
Chip Control During Turning
Efficient chip control is important for safe and consistent CNC turning. Long, uncontrolled chips can interfere with the cutting process, damage surfaces, or create handling problems.
Tool geometry, cutting parameters, coolant, and chip-breaker design can all influence chip formation. The best approach depends on the workpiece material and machining operation.
Coolant and Lubrication
Coolant can help manage heat, improve tool life, and assist with chip evacuation in suitable applications.
However, coolant is not required in every turning operation. Its use should be based on the material, cutting tool, machining parameters, and manufacturer’s recommendations.
Maintaining Cutting Accuracy
Consistent cutting results depend on more than the CNC program. Tool wear, spindle runout, machine rigidity, thermal expansion, workholding, and setup accuracy can all influence the finished component.
Regular inspection and appropriate tool-offset adjustments can help maintain dimensional consistency during production.
Combining Multiple Operations
Modern CNC lathes can often perform several cutting operations in a single setup. A component might be faced, rough-turned, finish-turned, drilled, grooved, and threaded without being removed from the chuck.
Reducing the number of setups can save time and reduce the possibility of alignment errors between operations.
Conclusion
CNC lathe cutting operations provide manufacturers with a versatile range of methods for producing rotational components. Facing, turning, boring, drilling, threading, grooving, parting, chamfering, tapering, and contouring each serve different purposes within the machining process.
JSWAY operates within the CNC machinery sector, but regardless of machine manufacturer, successful turning depends on selecting suitable tools, cutting parameters, workholding methods, and machining strategies. Understanding each operation makes it easier to develop efficient processes and achieve consistent finished-part quality.